21.1 Introduction
- • In this lecture, we present the process technologies associated to Butadiene and Toluene.
• Butadiene manufacture is considered using n-Butane as the feed stock.
• Benzene process technology refers to the famous hydrodealkylation process that uses toluene as the feed stock.
• We first present the process technology associated to Butadiene.
21.2 Butadiene
21.2.1 Reactions
- • Main reaction: n-Butane → Butadiene + Hydrogen.
• Side reaction: n-Butane → n-Butylene + Hydrogen.
• Catalyst: Chromium oxide on alumina.
• Coke deposition is a very important issue. Therefore, catalyst regeneration needs to be carried out very frequently.
• Reaction is exothermic.
• Operating conditions: 650°C and 120-150 mm Hg (low pressure).
• Feed stock: n-Butane with some isopentane from refinery processes.
21.2.2 Process Technology (Figure 21.1)
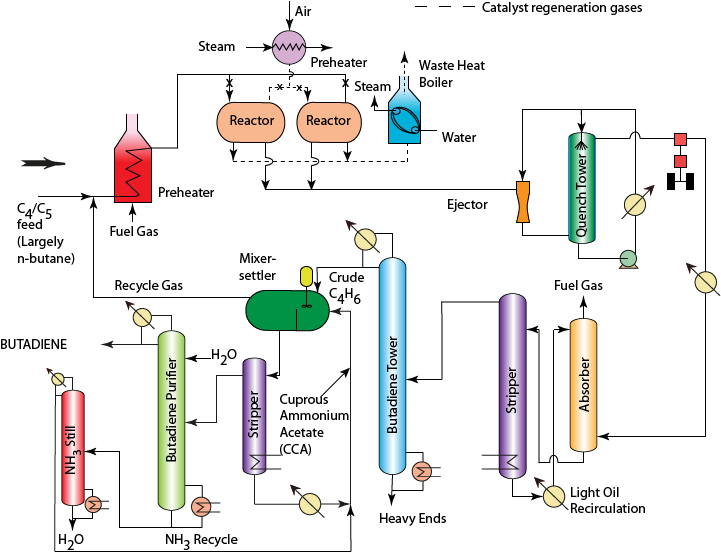 |
Figure 21.1 Flow sheet of Butadiene manufacture
- • The process technology for Butadiene manufacture consists of a reactor-separator-recycle system.
• The separation network is extremely complex and involves quenching, absorption, distillation and extractive distillation process.
• First, the feed stock is pre-heated in a furnace along with unreacted gases that have been recovered in the process using the separator network.
• After pre-heating in a furnace to desired temperature, the gases enter the catalytic packed bed reactors loaded with the catalyst.
• After the specified residence time, the product is withdrawn and the feed to the unit is stopped. The product withdraw and stoppage of the feed flow to the reactor unit is carried out using valves.
• The coked catalyst is subjected to combustion using pre-heated air. Air pre-heating is done using steam in an extended area heat exchanger equipment. Therefore during regeneration, another set of valves operate to allow the pre-heated air in and enable the product withdrawal after the combustion.
• The pre-heated air not only removes the coke as CO2 but increases the reactor temperature to 650°C.
• The flue gases are sent to a waste heat recovery boiler so as to generate steam from water.
• The entire operation of a feed entry, product withdrawal, pre-heated air entry and combustion gases withdrawal from the packed bed reactor corresponds to one single cycle.
• Since the above operation is a batch operation, to make the operation continuous in accordance to the separation network, two reactors are used and these reactors are operated in cyclic fashion i.e., when the first reactor is subjected to reaction, the second reactor is subjected to catalyst regeneration and vice-versa.
• The hot reactor outlet gases are sent to a quenching operation where light gas oil is used to quench the gases using a recirculating quenching tower.
• After product gases from the quenching tower are compressed and cooled to enter an absorber.
• In this absorber, naphtha is used as an absorbent to absorb all hydrocarbons except fuel gas.
• The absorbent + hydrocarbons enter a stripper that produces fresh naphtha and hydrocarbon mixture. The hydrocarbon mixture consists of unreacted feed stock and butadiene and some heavy ends.
• This mixture now enters a fractionator to separate the crude butadiene and heavy ends.
• The crude butadiene consists of butadiene and unreacted feed stock i.e., n-butane and isopentane. The separation of n-butane, other hydrocarbons with butadiene is one of the difficult separations and they cannot be separated using ordinary distillation. Therefore, a complicated route of separation is followed next that involves azeotropic distillation using ammonia.
• The crude butadiene is mixed with ammoniated cuprous ammonium acetate solution in a mixer settler. This solution is generated by absorbing ammonia into fresh cuprous ammonium acetate solution.
• The ammoniated cuprous ammonium acetate is sent to a mixer settler unit where the butadiene dissolves in the ammoniated solution. The gas from the mixer settler unit is recycled to mix with the feed stock and enter the pre-heater.
• The ammoniated cuprous ammonium acetate solution is thereby stripped to separate butadiene + ammonia from the ammonium acetate solution. The regenerated fresh solvent is allowed to absorb NH3 and thereby enter the mixer-settler unit.
• The ammonia + butadiene mixture enters a fractionator fed with water. Here, water interacts with ammonia and generates the ammonium hydroxide product as the bottom product and butadiene is obtained as the top product.
• The ammonia solution is subjected to stripping to separate water and ammonia. The water is recycled back to the butadiene purifier and ammonia is allowed to get absorbed into the fresh cuprous ammonium acetate solution.
• This process is not followed in India . In India, it is manufactured from ethanol by catalytic cracking at 400-450°C over metal oxide catalyst.